
 English

News
Thu 10 , 2026
Two suppliers can quote the same part and come back with numbers that differ by a factor of three. That gap is usually not a markup — it is a difference in what each quote includes, what steel it assumes, how many cavities it plans, and how much of the Design risk the Toolmaker is carrying. This guide explains why injection mold quotes diverge, and how to compare them line by line so the cheapest number does not turn into the most expensive decision.
When two quotes for the same drawing come back far apart, the difference is almost always in one of five places, and none of them is visible on the quotation page.
Steel source and grade. A locally sourced pre-hardened steel and an imported hardened tool steel can differ in price by several times, and in tool life by more than that. Both quotes can honestly say “steel mould”.
What the price includes. A quote that excludes design, mold flow analysis or the trial run is not cheaper — it is a partial price. Compare the total, not the headline.
Machining method. Wire cutting, precision EDM and hand fitting take time. A quote that assumes faster, less precise methods will be lower, and the gap tends to show up at the first trial.
Heat treatment. Hardening a cavity extends tool life substantially. If one quote hardens and the other does not, the cheaper tool may be the more expensive decision over a production life.
Lead time. An expedited tool carries overtime and reshuffled capacity. A quote that promises a much shorter lead time at a lower price is worth questioning.
An injection mold quote is not one item. It is a bundle of six or seven cost blocks, and the fastest way to misread it is to treat it as a single number. A complete custom injection mold quote normally itemises:
| Cost block | What it covers | Commonly excluded |
|---|---|---|
| Design and analysis | Part review, DFM feedback, gating and cooling layout, mold flow analysis | Often quoted separately or skipped |
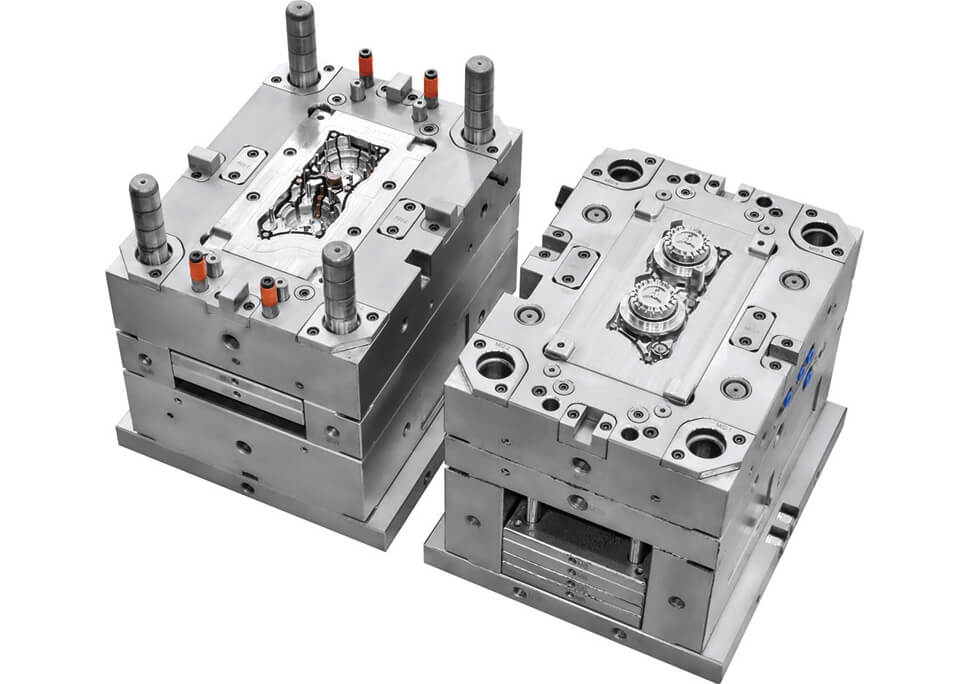
| Steel and standard components | Mould base, cavity and core steel, ejector system, slides, lifters, hot runner | Grade upgrades, imported steel |
| Machining | CNC roughing and finishing, EDM, wire cutting, deep-hole drilling, fitting hours | Extra fitting after the first trial |
| Heat treatment and finishing | Hardening for long-life tools, polishing, texture, engraving | Hardening on lower-priced tools |
| Trial run and samples | Mounting the tool, setting the process, producing the first shots | Second and third trials |
| Measurement and documentation | Dimensional inspection of the first article and the report that goes with it | CMM reports, material certificates |
If you want the absolute cost ranges rather than the structure, our guide to how much a custom injection mold costs breaks the numbers down by complexity, material and cavity count.
Part design is the single largest lever on tooling cost, and it is the one most often frozen before anyone with tooling experience sees it. Four design decisions move the number the most:
Undercuts. Any feature that cannot be released in the line of draw needs a slide, a lifter or a collapsing core. Each mechanism adds machining hours, adds moving parts that can wear, and adds failure modes. Removing a single unnecessary undercut can take a meaningful percentage off a tool price.
Wall thickness. Uniform walls cool evenly and shrink predictably. Abrupt thickness changes create sink marks, warpage and internal stress, and they force the toolmaker to add cooling where the geometry does not naturally allow it.
Draft. Insufficient draft means the part drags on ejection, which shows up as scuffing and, in bad cases, as a tool that has to be re-cut. Draft is free to add on the drawing and expensive to add later.
Gate location. Where the plastic enters determines flow length, weld line position and how much pressure the tool needs. On cosmetic or structural parts the gate position is a design decision with a tooling consequence, not a detail to leave to the shop floor.
This is the work that happens in the design review, before any steel is ordered. A supplier who runs a proper DFM review on your part is not adding a step — they are reducing the chance that the mould has to be modified after the first trial. You can see how that review feeds into the tool in our injection mould design service.
Mould cost and part cost pull in opposite directions, and the volume target decides where the balance should sit.
At low volumes, the mould is the dominant cost and the sensible move is a simple, single-cavity tool that gets you to market. The tool is cheap, the unit cost is high, and the moulding cost is a small part of a small number. At high volumes, the mould cost is amortised over so many parts that the cavity count should be driven by unit cost: a four or eight cavity tool costs more up front but can cut the cost per part by a multiple.
The mistake is to buy the tool for the volume you have today when the volume you expect in eighteen months is five times larger. The second mistake is the opposite: building an eight-cavity tool for a product that never gets past its first order. If your program starts small and scales, read our guide to low volume injection molding for how to structure the tool and the production plan so the first tool does not become dead capital.
Ask every supplier for the same breakdown, then compare line by line. The following items are the ones that decide whether two numbers are actually comparable:
| Ask for | Why it changes the comparison |
|---|---|
| A line-item breakdown | Design, steel, machining, finishing and trial priced separately |
| Cavity count stated explicitly | A single-cavity and a four-cavity quote are not the same product |
| Steel grade and source | Sets the tool life and the repair cost later |
| Expected mould life in shots | Converts a one-off price into a cost per thousand parts |
| Whether DFM and mold flow are included | Determines who finds the design problems, and when |
| Number of trials and sample quantity | One trial versus three is a real difference in scope |
| Mould ownership and handover | You should own the tool and be able to move it |
A toolmaker who can answer all seven of these in writing is telling you something about how the tool will be built. One who cannot is asking you to compare prices on faith.
Most of the spread between quotes comes from what each supplier was asked to assume. If you send the same information to every toolmaker, the quotes converge and the comparison becomes meaningful. The package that produces a comparable custom injection mold quote contains:
The 3D model. STEP or IGES, at the revision you actually want quoted.
The 2D drawing with tolerances. A model alone does not state which dimensions are critical, and critical dimensions are where the tooling hours are.
The material grade, not just the family. “PP” and a specific PP grade with a stated filler and melt flow are not the same tooling proposition.
Expected annual volume and product life. This is what tells the toolmaker whether to propose a single-cavity or a multi-cavity tool, and whether hardening is worth the cost.
Cosmetic and surface requirements. Texture, gloss level and visible-surface classification belong in the brief, because polishing and texturing are priced, not given.
Target tool life in shots. A 100,000-shot tool and a 1,000,000-shot tool are different pieces of engineering, and the quote should reflect the one you asked for.
Send that package to three suppliers and you will get three quotes that can actually be read side by side. Send a single sentence and you will get three different guesses — and an injection mold quotation you have no way of comparing to anything.
The two numbers that matter are the mould cost and the unit cost at your target volume, and they have to be judged together. A cheaper tool with fewer cavities can be the right answer at ten thousand parts a year and the wrong answer at half a million, because the saving on the tool is paid back many times over in cycle time and labour on every part.
Convert every quote into a cost per part at your real annual volume before you compare. That single step removes most of the confusion created by headline tooling prices.
YouKing Mould has built injection moulds in Dongguan, China since 2006, producing 300 to 400 moulds a year with 5,500 square metres of floor space and 27 injection moulding machines. Design, steel cutting, EDM, fitting, trial run and measurement all happen in the same facility, which means a quote from us can be itemised against real machine hours rather than estimated.
Our custom injection mould tooling page shows the range of tools we build, from automotive structural components to multi-cavity medical parts. If you want the design side first, the mould design and DFM review is where a project usually starts.
An injection mold quote is not a price you negotiate down; it is the sum of design decisions, steel choices, cavity count and scope. Read it as a scope document rather than a number, ask for the same breakdown from every supplier, and compare the cost per part at your real volume. That is how you get an accurate injection mold quote instead of a cheap one.
Send us your 3D file, the drawing with its tolerances, your target material grade and your expected annual volume. We will run the DFM review, propose a cavity layout and cooling design, and give you a line-item tooling quote plus a unit cost at your volume — so you can compare it properly against the other quotes on your desk.
We attach great importance to the customers' demands for product quality and rapid production.
We always believe that meeting the customers' needs is the realization of our value!