
 English

News
Wed 10 , 2026
Every drawing that comes into a mold shop carries tolerances, and a surprising number of them are impossible. Not because injection molding is inaccurate — a well-built Tool holds dimensions that would surprise most machinists — but because the tolerance is often written on the wrong dimension, or written without knowing what the process controls. The result is a quotation that is either padded or wrong, and a first article report full of red numbers that were never achievable in the first place.
This guide explains how injection molding tolerance actually works: what the standard grades mean, what a custom tool can realistically hold, where molding differs from machining, and how to specify tolerances that a mold shop can meet without adding cost you do not need.
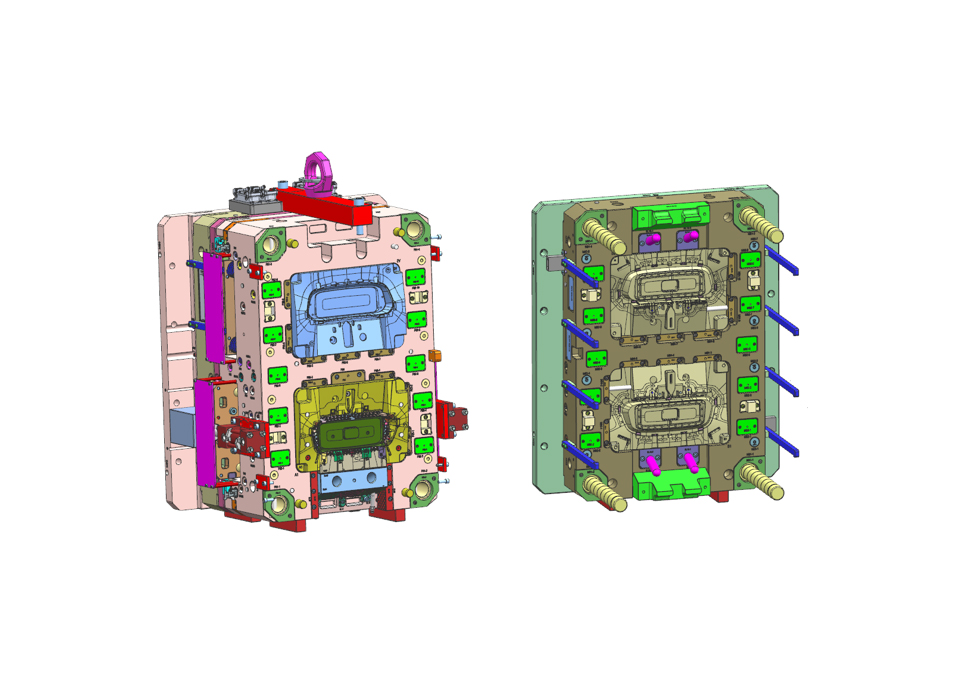
An injection molding tolerance is the permitted variation on a dimension of a moulded part. It has to absorb three separate sources of variation, and understanding them is what makes the difference between a realistic tolerance and a wish.
Tool variation. The cavity and core are machined to a tolerance themselves. Whatever the steel is cut to is baked into every part the tool will ever make.
Material shrinkage. Resin shrinks as it cools, and it does not shrink equally in all directions. Shrinkage varies with grade, with wall thickness, with gate position and with the process window.
Process variation. Melt temperature, hold pressure, cooling time and mold temperature all move dimensions slightly from shot to shot, and more than slightly from one machine to another.
The tolerance on the drawing has to cover all three. That is why the same nominal dimension can be a routine tolerance in one material and a difficult one in another.
Injection molding tolerance standards exist precisely because a single plus/minus figure cannot describe every size. The most widely used framework for moulded plastics is the German standard DIN 16901, which divides tolerances into groups by material behaviour and then into grades by nominal size. Similar tables appear in ISO and in most national standards, and Chinese mold shops work to them daily.
| Grade | Typical use | Practical meaning |
|---|---|---|
| General tolerance (DIN 16901 group 130/140) | Non-critical dimensions, no mating function | The default when nothing else is specified; cheap and normally sufficient |
| Medium tolerance | Dimensions that affect assembly but not fit-critical features | Achievable on any well-built tool with a stable process |
| Tight tolerance | Mating features, snap fits, sealing surfaces | Requires good tool steel, stable cooling and a controlled process window |
| Precision tolerance | Optical, medical and precision mechanical interfaces | Requires a dedicated tool, a validated process and often 100% inspection |
The practical rule behind all of these tables is the same: tolerance grows with size. A 5 mm dimension can be held far more tightly than a 300 mm dimension, because shrinkage variation scales with length.
The honest answer to what tolerance can injection molding hold depends on the dimension and on the direction. The chart below is the working range we quote on custom tools; treat it as a plastic molding tolerance chart for planning, not as a guarantee, because the resin and the part geometry always have the final say.
| Dimension | Typical achievable tolerance | Tight tolerance, controlled process | Notes |
|---|---|---|---|
| Up to 10 mm | ±0.05 mm | ±0.02 mm | Small dimensions follow the steel; the tool dominates |
| 10–50 mm | ±0.10 mm | ±0.05 mm | The normal working range for most engineering parts |
| 50–150 mm | ±0.20 mm | ±0.10 mm | Shrinkage variation starts to dominate |
| 150–300 mm | ±0.35 mm | ±0.20 mm | Warpage, not shrinkage, becomes the limiting factor |
| Over 300 mm | ±0.50 mm or by agreement | Part-specific | Requires a warp study and often a compensated tool |
Two dimensions behave differently from everything else. Dimensions formed by a single steel feature — a hole diameter, a boss diameter, a slot width — are much more repeatable, because they are set by the tool rather than by shrinkage. Dimensions that span across a flow path, or that are measured after the part has cooled and warped, are the ones that cause arguments. If a drawing has a tight tolerance, it should be on a feature the tool controls, not on an overall dimension the process controls.
Buyers used to machined parts often assume injection molding tolerance vs machining is a simple quality gap. It is not. Machining is a subtractive process: the tool moves to a position and cuts, so the achievable tolerance is a property of the machine, and holding ±0.01 mm is routine.
Molding is a replication process. The cavity is the precision instrument and it can be machined as accurately as any part. What you cannot control as tightly is the transformation of molten resin into a solid, because the material changes size as it cools and does so unevenly. So the comparison is not "molding is less accurate". It is:
Machining holds a tight tolerance on every part, at a cost per part.
Molding holds a tight tolerance on the tool, and a looser one on the material, at a very low cost per part once the tool is paid for.
When a feature genuinely needs machined accuracy — a sealing face, a bearing seat, a thread that must gauge — the usual answer is to mould close and finish by machining, not to demand the tolerance from the mould.
That last option is worth pricing early. A moulded part plus a light secondary machining operation is frequently cheaper than a tool engineered to hold a tolerance the process cannot repeat, and it removes the risk of a tool that never quite passes its own first article inspection. Our precision mold components capability exists for exactly this reason.
Tight tolerance injection molding is not bought with a better machine alone. It is Designed in, in this order:
Start with the material. An amorphous resin such as PC or ABS shrinks less and more predictably than a semi-crystalline resin such as POM or PA. If the tolerance is critical, the resin choice matters as much as the tool.
Fix the wall thickness. Variable wall thickness is the single most common cause of a dimension that will not repeat.
Design cooling for balance, not for speed. Uneven cooling produces uneven shrinkage, which produces warpage, which destroys overall dimensions.
Place the gate so that the tight dimensions are close to it. Dimensions near the gate are set by the tool; dimensions at the far end of the flow are set by the process.
Build the tool with the shrinkage allowance verified on a trial, not taken from a table. A trial shot and a measured shrinkage value is worth more than any data sheet.
Lock the process. A tight tolerance that depends on a specific operator adjusting a setting will not survive a machine change.
When a custom injection molding tolerance is missed, the cause is almost always one of five things, and they are worth checking in this order: the shrinkage allowance in the tool, the gate position and cavity balance, the cooling layout, the process window, and the part design itself. Of those five, only the last two can be changed after the tool is cut — which is why the design review matters so much on a tight-tolerance project.
Warpage deserves a separate mention because it is so often mistaken for a shrinkage problem. A part can be perfectly on dimension and still be rejected because it is twisted or bowed, and no amount of steel adjustment fixes it if the cause is unbalanced cooling. We cover the causes in detail in our guide to why injection molded automotive parts warp.
The best way to handle tolerances for injection molded parts is to stop treating every dimension as equally important. A workable specification looks like this:
Put a general tolerance note on the drawing and leave most dimensions to it.
Mark the dimensions that genuinely matter — the ones that touch another part, seal, snap or locate — and give only those a tight tolerance.
Say which dimensions are measured before and which after a defined settling period, because a part measured hot and a part measured after 24 hours are different parts.
State the datum scheme, so the mold shop and your incoming inspection measure from the same place.
Agree the resin grade in writing. A tolerance without a material is not a specification.
If a tolerance turns out to be unachievable, the right response is to change the design or add a secondary operation, not to accept a tool that will produce rejects for its whole life. That conversation is much easier to have before the tool is cut, which is what a DFM review is for — see how to make injection mold tooling that performs for what that review covers.
Youking Mould builds custom injection molds and Precision Components in Dongguan, with mold design and mold flow analysis, tooling and injection production under one roof. On a tight-tolerance project that combination matters: the shrinkage allowance is verified on our own machines, the first article is measured on our own inspection equipment, and any correction is made by the same engineers who designed the tool.
If you have a drawing with tolerances you are not sure the process can hold, send it to us with the 3D file, the resin grade and the annual volume. We will tell you which dimensions are realistic as drawn, which ones need a different gate position or wall thickness, and which ones are better moulded close and finished by machining — before you commit to a tool. You can see the full range of what we build on our custom injection mold tooling page, or read what to consider before ordering a custom injection mold for the commercial checklist.
Injection molding can hold tolerances of a few hundredths of a millimetre on small, tool-controlled features, and around ±0.2 mm on a dimension of 100 mm once shrinkage and warpage are allowed for. The number is not fixed by the machine; it is fixed by the material, the wall thickness, the cooling design and the gate position — all of which are decided before the steel is cut.
Specify a general tolerance for the whole drawing, reserve tight tolerances for the features that genuinely interface with something else, and confirm the resin in writing. Then let a DFM review tell you whether the tight ones are achievable, because that is the point at which changing them is still free.
We attach great importance to the customers' demands for product quality and rapid production.
We always believe that meeting the customers' needs is the realization of our value!